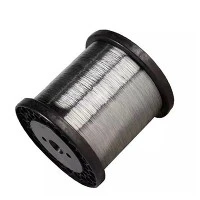
Product Introduction
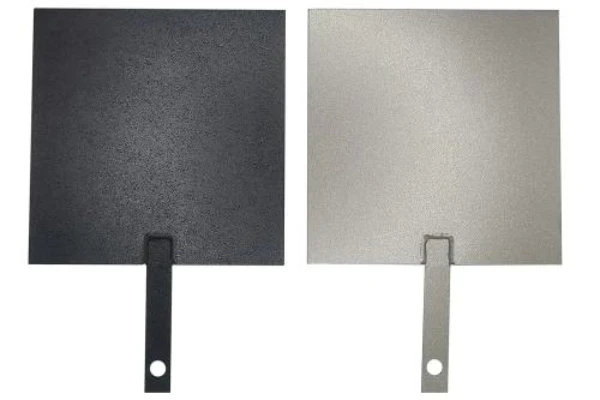
In many electrolysis systems, anodes wear out too soon or lose stability under acid and chlorine exposure. The OEM Titanium Anode is designed to handle these harsh conditions by combining a pure titanium base with a durable Ru–Ir oxide coating. It keeps voltage stable, resists corrosion, and minimizes replacement frequency. Commonly used in acid recovery, marine cooling, and chemical treatment systems, it offers dependable long-term performance with less maintenance.
Product Parameter
|
Specification |
Typical Value |
Benefit / Value to User |
|
Base Material |
ASTM Gr1 / Gr2 Titanium |
Strong foundation for coating adhesion |
|
Coating Type |
Ru–Ir Mixed Oxide (MMO) |
Excellent resistance to acid and chlorine |
|
Current Density |
50–300 A/m² |
Flexible for pilot and industrial operation |
|
Surface Potential |
1.2–1.5 V vs Ag/AgCl |
Lower running voltage, reduced energy cost |
|
Operating Temperature |
≤80°C |
Works well in acidic or chloride media |
|
Service Life |
8000–12000 hours |
Fewer replacements, less downtime |
|
Suitable Medium |
pH 1–4, Cl⁻ ≤30 g/L |
Stable under strong acid and saline exposure |
Product Features & Application
■ Built for Harsh Electrolytic Environments:
The Ru–Ir coating shields the titanium substrate from acid erosion and oxidation, keeping current flow stable even in aggressive chemical media.
■ Uniform Current Flow:
Every OEM Titanium Anode undergoes controlled thermal oxidation to achieve consistent coating thickness and even current distribution.
■ Low Maintenance, High Efficiency:
The smooth oxide surface minimizes fouling, making cleaning easier and reducing the need for frequent shutdowns.
■ Versatile Industrial Use:
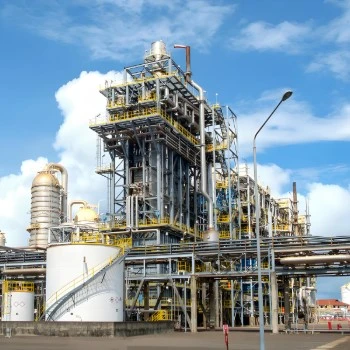
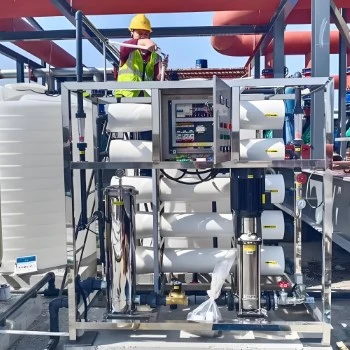
Widely applied in acid regeneration, electrochemical oxidation, seawater treatment, and chemical manufacturing systems.
Product Details

■ Titanium substrate available in Grade 1 or Grade 2.
■ Ru–Ir mixed oxide coating sintered at ~480°C.
■ Matte, uniform surface for steady voltage performance.
■ Concentricity tolerance ≤0.05 mm for current balance.
■ Plate, mesh, or tubular configurations available.
■ Optional welded or threaded connection ends.
After-Sales Service

why choose our products
■ 24-hour response for technical and commercial inquiries.
■ 12-month coating integrity guarantee with lifetime support.
■ Remote installation and maintenance assistance.
■ Material and current density selection guidance.
■ Pre-delivery inspection for adhesion and conductivity.
■ Custom production from prototypes to bulk orders.
FAQ
Q1: How long can the anode last in acidic media?
A: Typically 9000–12000 hours under pH 2 and 100 A/m². This means fewer maintenance stops and lower operating costs.
Q2: Can it handle acid cleaning or chloride wastewater?
A: Yes. The Ru–Ir coating stays stable in such media, ensuring long-term performance and reduced cleaning chemical use.
Q3: Which titanium grade should I choose?
A: Gr1 suits light acid use; Gr2 is for high pressure or long operation. We can help recommend the right option.
Q4: Is third-party testing available?
A: Yes, SGS or equivalent lab verification can be arranged for coating and adhesion testing.
Q5: Any installation advice?
A: Avoid over-tightening or impact on coated areas; ensure stable contact with conductive parts.

Company profile
Baoji Zhongxinbao Metal Materials Co., Ltd. specializes in titanium and MMO anodes for marine, chemical, and industrial systems. We integrate extrusion, coating, and machining under one facility to ensure stable quality and flexible customization. Each anode is inspected for adhesion and voltage performance before delivery. With reliable production capacity and technical experience, we supply OEM clients worldwide with durable and efficient OEM Titanium Anode solutions.
we are here for you
Hot Tags: oem titanium anode, China oem titanium anode manufacturers, suppliers, factory, MMO Titanium Anode, special application titanium anodes, Titanium Anode For Electrolytic Copper Foil